The chemical properties of cotton come from its cellulose structure: accessible hydroxyl groups attract water and support dyeing, acids hydrolyze its chains, controlled alkalis promote swelling, and excessive oxidation reduces strength. For industrial textile buyers, these reactions help explain how preparation and finishing turn cotton into a workwear fabric with specified performance.
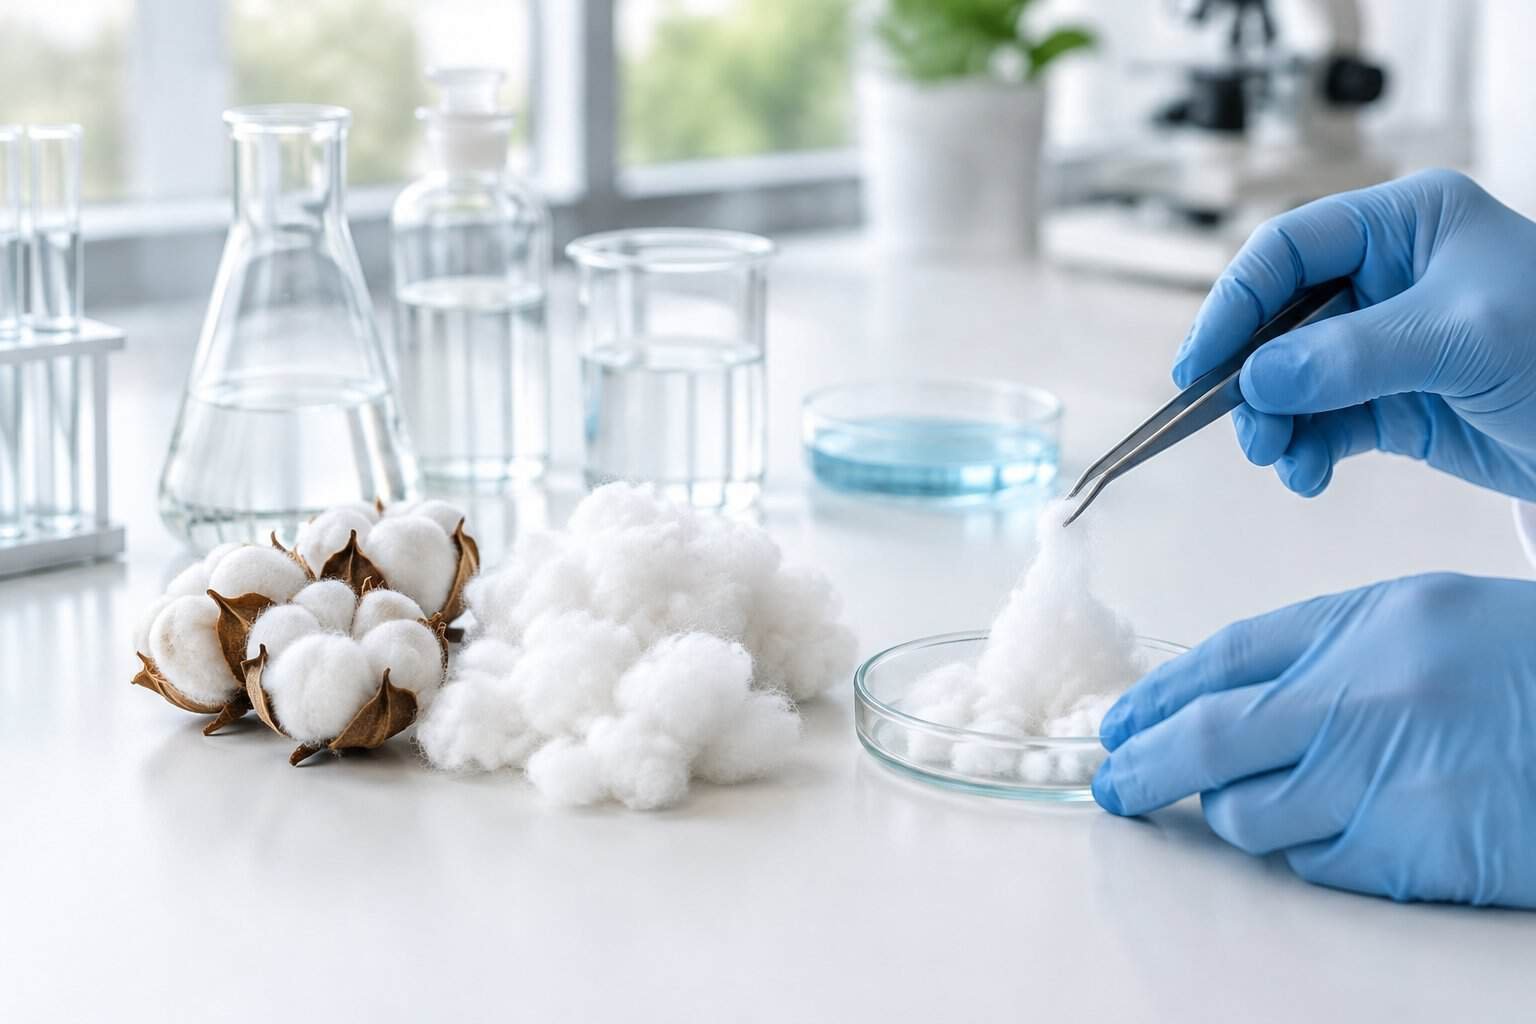
The textile industry uses cotton’s chemical reactivity to improve absorbency, develop consistent shades, and apply functional treatments. A purchasing specification becomes more useful when it separates the fiber’s inherent characteristics from the properties introduced during manufacturing.
Protective workwear adds another requirement: evidence tied to the finished fabric and garment. Cotton chemistry explains processing behavior; relevant performance tests establish suitability for a defined workplace exposure.
How Does Cotton Respond to Chemicals?
Cotton responds well to controlled textile preparation, while acids and excessive oxidation damage its cellulose chains. The chemical properties of cotton fiber also influence measurable physical properties of cotton, including wet strength, swelling, and dimensional behavior.
Property Table: Chemical Response and Processing Implications
The following responses describe cotton as a cellulosic substrate. Actual fabric behavior also reflects its construction and processing history. A chemical response alone establishes neither wearer protection nor service life.
| Chemical exposure or condition | Cotton’s response | Processing implication |
|---|---|---|
| Water after effective scouring | Wetting, absorption, and fiber swelling | Supports uniform application of aqueous dyes and finishes |
| Acids | Hydrolysis of cellulose chains | Requires controlled exposure and removal of acidic residues |
| Controlled alkalis | Comparatively good resistance, with swelling under suitable conditions | Enables scouring and mercerization |
| Oxidizing agents | Removal of natural coloring matter; cellulose damage under excessive exposure | Requires controlled bleaching and retained-strength assessment |
| Reactive dyes | Bond formation at accessible cellulose hydroxyl groups | Requires suitable fixation and thorough wash-off |
| Strong heating or flame | Decomposition, charring, and combustion | Requires engineered flame-retardant treatment for relevant protective applications |
Inherent Fiber Properties vs. Applied Finishes
Cellulose gives cotton its underlying affinity for moisture and its characteristic chemical responses. Applied treatments introduce additional functions, such as liquid repellency or modified burning behavior. The practical limits of cotton’s resistance to chemicals therefore require separate consideration from the performance of a finished protective garment.
How Does Cellulose Structure Affect Water Absorption?
Cotton absorbs water through accessible hydroxyl groups and a porous fiber structure that supports capillary movement. Surface cleanliness determines how readily liquid reaches those internal sorption sites.
Cotton Composition and Fiber Layers
Cotton fiber develops as a seed hair on the cotton plant, which belongs to the genus Gossypium. The chemical composition of cotton includes cellulose alongside waxes, pectins, proteins, and smaller noncellulosic fractions such as hemicellulose. After scouring and bleaching, cotton is 99% cellulose.
Its outer cuticle covers the primary wall, while the secondary wall forms most of a mature fiber’s mass. This secondary cell wall contains densely arranged cellulose fibrils surrounding the lumen, the central canal left as the fiber matures. Spaces between fibrils provide pathways for liquids and water vapor.
Cellulose Chains, Hydroxyl Groups, and Hydrogen Bonding
Cotton cellulose consists of long glucose-based chains joined by glycosidic bonds. The degree of polymerization describes chain length, which contributes to fiber strength alongside molecular organization. Closely packed crystalline regions restrict access, while less ordered regions provide greater accessibility.
Hydroxyl groups on the cellulose polymer form hydrogen bonding interactions within and between chains. Accessible groups also interact with water molecules. This combination explains cotton’s hydrophilicity without implying that every part of the fiber is equally accessible to moisture.
Why Scouring Changes Wettability and Moisture Uptake
Raw cotton’s waxy surface limits initial wetting despite the hydrophilic cellulose beneath it. Scouring removes oils, waxes, pectins, and other noncellulosic materials, exposing a more readily wetted surface. Effective rinsing removes the loosened material and processing chemicals.
Wettability describes how readily liquid spreads and enters the fabric. Moisture content also reflects atmospheric humidity and the fiber’s ability to sorb water vapor. A rapid wetting result therefore addresses a different property from equilibrium moisture uptake.
Why Do Acids Weaken Cotton?
Acids weaken cotton by catalyzing hydrolysis of the bonds connecting its cellulose units. Shorter chains reduce the fiber’s ability to carry load.
Acid Hydrolysis and Cellulose Chain Breakdown
Acid hydrolysis breaks glycosidic linkages within the cotton fibre. As chain length falls, fiber strength declines and the material becomes tender. Early damage requires mechanical testing to assess because appearance alone provides an incomplete indication of retained strength.
Acidic residues left in fabric deserve particular attention before drying or heated finishing. Their continued presence extends exposure beyond the intended processing stage. Controlled rinsing and a suitable industrial finishing sequence help limit that exposure.
How Exposure Conditions Affect Fiber Damage
Acid identity, concentration, temperature, and contact time jointly determine the extent of damage. Hot conditions accelerate hydrolysis, while concentrated or prolonged exposure increases the risk of substantial strength loss. Mild processing acidity still requires a defined purpose and controlled conditions.
For workwear, a chemically stained area warrants assessment under the employer’s contamination procedure. Domestic neutralization attempts introduce additional reactions and provide no reliable evidence of restored protection. Replacement decisions should follow the garment manufacturer’s instructions and the workplace hazard assessment.
How Do Alkalis Affect Cotton During Processing?
Cotton’s comparatively good resistance to alkalis enables established industrial processes such as scouring and mercerization. Swelling and chemical damage remain separate outcomes that depend on the treatment conditions.
Comparatively Good Alkali Resistance Under Controlled Conditions
The cellulose backbone tolerates many controlled alkaline textile treatments. This alkali resistance allows processors to remove impurities and support dye fixation while retaining useful strength. A properly managed alkaline bath therefore serves a productive role in cotton manufacturing.
Fabric compatibility also includes any blend fibers, colorants, and existing finishes. An alkaline process suited to untreated cotton requires separate assessment when the fabric carries a functional treatment. Finished-fabric testing captures the combined result.
Swelling and Industrial Mercerization
Mercerization uses controlled sodium hydroxide treatment to swell cotton and alter its internal structure. Under suitable conditions, it converts cellulose I toward cellulose II and changes fiber cross-sectional shape. Industrial mercerization also improves dyeability and increases water sorption.
Tension control influences luster and dimensional behavior during treatment. Slack processing permits contraction, while tensioned processing restrains dimensional change. Subsequent washing and finishing influence residual fabric shrinkage in the completed workwear material.
How Temperature, Concentration, Time, and Oxidation Affect Damage
Alkali tolerance has practical limits shaped by concentration and temperature. Contact time adds another exposure variable, and oxidative conditions increase the risk of cellulose degradation. Changes in any of these conditions require assessment of the complete process.
Rinsing and controlled neutralization form part of industrial process management. Retained tensile or tear strength helps identify damage that a shade inspection would miss. Process approval should use the intended substrate and finishing sequence.
How Can Oxidants Damage Cotton?
Oxidants damage cotton when bleaching reactions extend from unwanted coloring matter to the cellulose itself. Excessive oxidation creates chemical changes that promote chain breakdown and loss of fiber strength.
Hydrogen Peroxide, Sodium Hypochlorite, and Sodium Perborate
Hydrogen peroxide is widely used for cotton bleaching under controlled conditions. Sodium hypochlorite is a chlorine-based oxidant, while sodium perborate releases peroxide in aqueous systems. Each requires a formulation suited to the substrate and intended result.
Peroxide bleaching requires attention to stabilization and metal contamination because uncontrolled decomposition promotes localized damage. Hypochlorite treatment also requires control of pH and residual oxidant removal. A bleach name alone provides insufficient information about its effect on a finished workwear fabric.
Oxidative Chain Damage During Bleaching and Finishing
Oxidation introduces carbonyl and carboxyl groups into cellulose and, under damaging conditions, causes chain scission. The resulting material loses strength even when its whiteness appears satisfactory. Localized catalytic reactions also produce uneven damage across the fabric.
Residual oxidants interfere with later processing, including some coloration and finishing systems. Effective rinsing and appropriate industrial removal steps reduce carryover. Strength testing after the complete sequence gives a more useful approval result than whiteness alone.
What Makes Cotton Suitable for Dyeing and Printing?
Cotton supports dyeing and printing because waterborne processing systems reach accessible cellulose regions and suitable dyes interact with the fiber. Consistent preparation establishes the foundation for even coloration.
Dye Access and Reactive Sites in Cellulose
A scoured cotton fiber admits aqueous dye solutions through its accessible pores and less ordered regions. Hydroxyl groups provide chemical reaction sites for fiber-reactive dyes. Dense crystalline regions offer less access to larger dye molecules.
Preparation defects create differences in local dye uptake. Residual size or wax produces uneven wetting, while inconsistent bleaching changes the background shade. Printing also requires controlled absorbency to maintain definition and uniform color yield.
Reactive Dyes, Vat Dyes, and Colorfastness
Reactive dyes form covalent bonds with cotton under suitable fixation conditions. Dye hydrolysis competes with fixation, so wash-off removes hydrolyzed and unfixed color. The finished shade requires evaluation after that cleaning stage.
Vat dyes follow a different route: they are reduced to a soluble form for entry into cotton, then reoxidized into an insoluble form within the fiber. Colorfastness depends on the selected dye and processing quality. Washing, rubbing, light, and the intended workwear care conditions require their own assessments.
How Fiber Maturity and Preparation Affect Shade Uniformity
Fiber maturity influences cellulose wall development and dye response. Immature fibers and nep formation produce visible pale flecks or uneven appearance after coloration. Mechanical preparation and raw-material consistency therefore affect the final shade alongside dye chemistry.
Mercerization improves the dyeing appearance of immature cotton under suitable processing conditions. It does not remove every defect introduced during fiber preparation or yarn manufacturing. Approval samples should represent the intended bulk preparation and finishing route.
Why Does Cotton Need Engineered Flame-Retardant Finishes?
Ordinary cotton is combustible, so protective applications require an engineered system with evidence appropriate to the hazard. Its thermal behavior alone establishes no flame-resistance rating.
Ordinary Cotton Burns Rather Than Melts
Cotton decomposes under strong heating and burns when ignition conditions are met. Its cellulosic structure behaves differently from melt-forming thermoplastic fibers. OSHA states that cotton clothing can ignite and continue to burn under workplace arc or flame exposure conditions.
The absence of melting describes only one aspect of thermal behavior. Burning duration and heat transfer remain important to injury risk. Fabric weight and construction also influence the exposure response.
How Applied Finishes Change Burning Behavior
Suitable flame-retardant treatments alter cellulose decomposition and promote protective char formation. A flame-retardant-treated fabric therefore gains its modified burning behavior from an engineered finishing system. Natural waxes and pectins provide no basis for claiming protective flame resistance.
Finish chemistry must suit the base fabric and production conditions. Application uniformity and curing influence the final result. Additional treatments require compatibility checks because combined finishes change the fabric system.
Why Protective Performance Requires Relevant Testing
Different thermal hazards require different performance evidence. A small-scale flame test measures specified burning characteristics; arc exposure and flash-fire garment performance require their relevant assessments. Claims should identify the method and the tested material.
Purchasing requirements should connect flame-retardant fabric testing to the intended application. Reports need to identify composition, construction, and any required laundering pretreatment. Garment design adds further variables, including seams and closures.
What Does Cotton Chemistry Mean for Industrial Workwear?
Cotton chemistry helps textile buyers specify processing quality and finish compatibility for industrial workwear. Protection claims require additional evidence addressing the actual exposure and completed garment.
Balancing Absorbency, Dyeability, and Processing Durability
Absorbency and dyeability support cotton’s use in workwear, particularly where comfort and consistent coloration are priorities. Processing must preserve sufficient strength for the intended construction. These physical properties of cotton remain sensitive to chemical damage accumulated during manufacturing.
A useful specification combines composition and fabric weight with retained strength, dimensional change, and colorfastness requirements. Functional finishes add further acceptance criteria. Samples should pass through the full production sequence before approval.
Chemical Repellency vs. Barrier-Based Chemical Resistance
Chemical-repellent finishing reduces surface wetting by specified liquids under defined conditions. Levitex produces chemical-repellent fabrics through post-treatment finishing on cotton, cotton/nylon (C/N), and cotton/polyester (CVC) base fabrics. These fabrics belong to a distinct protection category from barrier-based chemical-resistant materials.
OSHA describes permeation as chemical movement through a material at the molecular level, including movement without visible evidence. Selecting chemical-resistant fabric therefore requires chemical-specific consideration of permeation, penetration, and degradation. Repellency results do not establish equivalent barrier protection or interchangeable use cases.
Checking Finished-Fabric and Garment Performance
Approval should cover the finished textile and the garment features relevant to the hazard. Fabric reports need to match the purchased composition and construction. Seams, closures, and exposed interfaces require attention where liquid entry or thermal exposure is foreseeable.
Care conditions also form part of the performance specification. Requirements for washing flame-retardant fabrics should follow the approved treatment system and garment instructions. Any claimed retention of protection needs supporting results after the specified maintenance sequence.
Match Cotton Chemistry to Verified Workwear Performance
Cotton workwear performs best when its cellulose chemistry, processing route, and applied finishes are matched to documented requirements. Acid sensitivity and oxidative damage require process control, while absorbency and controlled alkali response support effective preparation and coloration.
Textile buyers evaluating FR fabric finishing or chemical-repellent options can contact Charlie@levitex.com with their base fabric and finishing requirements. The inquiry should identify the intended exposure, care conditions, and requested performance tests, with separate acceptance criteria for flame behavior and chemical-liquid repellency.
Frequently Asked Questions
The chemical properties of cotton explain its processing response, while finished-fabric testing establishes application-specific performance. The following distinctions help keep purchasing claims precise.
What is the difference between cotton’s physical and chemical properties?
The physical properties of cotton include strength, fiber dimensions, and moisture-related behavior; its chemical properties describe reactions such as acid hydrolysis and oxidation. The categories interact because chemical changes to cellulose alter measurable physical performance.
Why does cotton absorb water after scouring?
Scouring removes waxes and other surface materials that restrict wetting, allowing water to reach accessible cellulose hydroxyl groups. Capillary spaces within the fiber and fabric help move and retain the liquid.
Is cotton resistant to acids and alkalis?
Cotton is sensitive to acid hydrolysis and has comparatively good alkali resistance under controlled textile processing conditions. Concentration, temperature, contact time, and oxidation determine the risk of damage.
Does cotton melting or burning indicate flame resistance?
Neither melting behavior nor burning alone establishes flame resistance. Ordinary cotton decomposes and burns without thermoplastic melting, while protective claims require relevant test results for the finished material.
Can chemical-repellent cotton replace chemical-protective barrier clothing?
Chemical-repellent cotton provides a different function from chemical-protective barrier clothing, so substitution requires evidence that it meets the assessed hazard requirements. Surface repellency alone supplies no proof of resistance to molecular permeation or prolonged chemical contact.